
STATE-OF-THE-ART LABORATORY
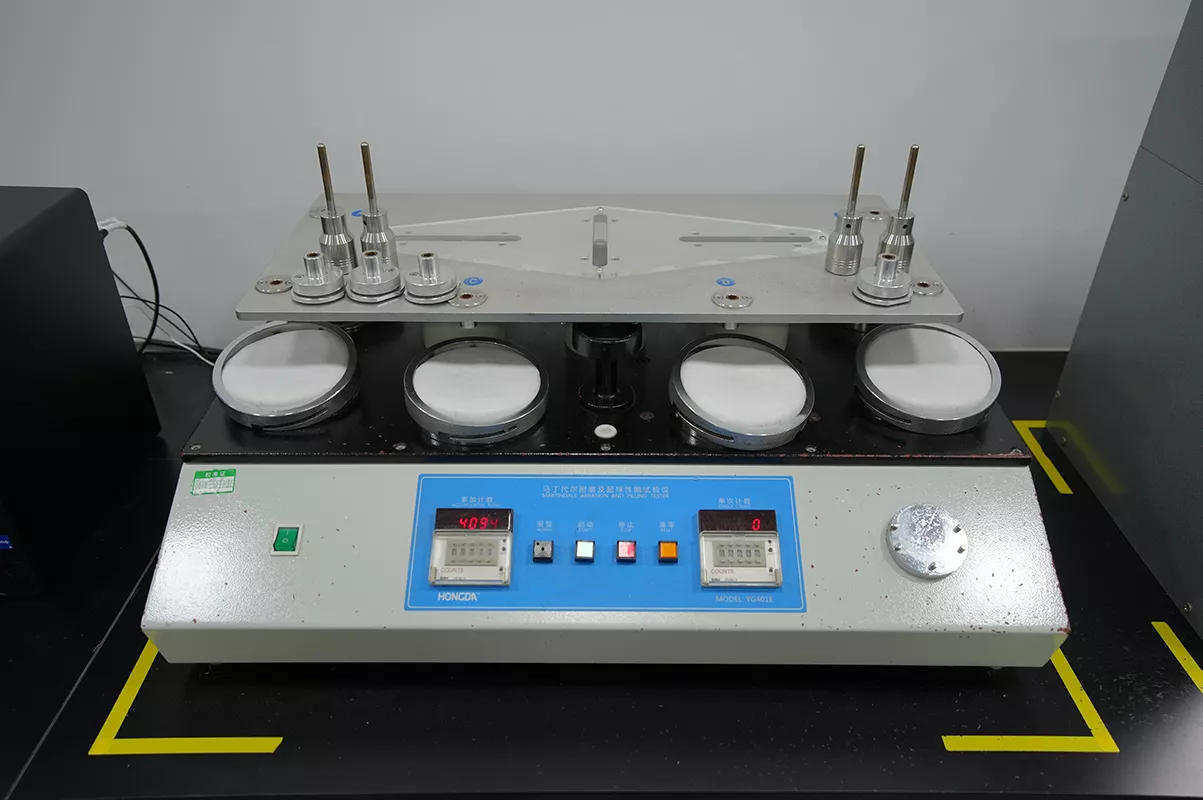
We don't just manufacture; we validate. Our in-house laboratory is equipped to conduct a wide range of testing, including microbial analysis, liquid absorbency (Wetback), and tensile strength. This helps verify that products meet international standards (ISO/ASTM) before they leave our facility.

Global Leading Production Technology
Operating 5+ advanced cross-laid spunlace lines (including imported ANDRITZ technology), we achieve an effective width of up to 3.2 meters. Our high-automation systems ensure precise weight control and uniform web formation.
Medical-Grade Cleanliness
Our workshop is built in accordance with GMP standards, featuring functional zoning, constant temperature and humidity control, and a smart purification system. This helps maintain a low-contamination environment for medical and hygiene products.

0
+Production Line
0
cmMaximum Effective Working Width
0
gMinimum Grammage
0
gMaximum Grammage
0
+Equipment
RIGOROUS QUALITY ASSURANCE (QA/QC)
Quality is data-driven. We continuously invest in advanced testing instruments to monitor key performance indicators


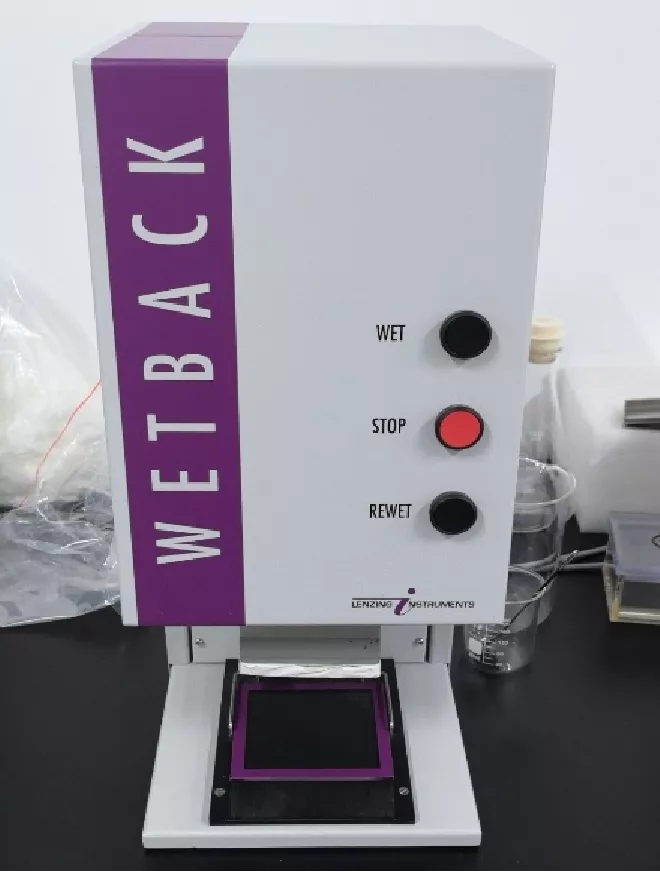 Liquid Strike-Through & Rewet Tester


Telephone:+86-513-86821106
Email:sales@jsjhnonwoven.com
Address:No. 199 Yuwanzhong Road, Shigang Industrial Park,
Tongzhou District, Nantong City, Jiangsu Province,
China.(Near Shanghai Port)


